PerMix Mayonnaise Production
PerMix News
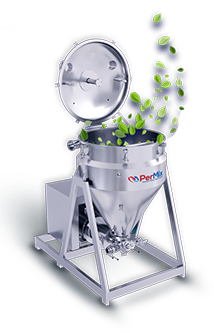

A dry starch may represent only a small percentage of a sauce or dressing formula, yet it can determine whether the batch meets specification. When powder enters the vessel poorly, it wets on the outside, traps dry material at the center, and forms fish eyes that high shear cannot always remove. For manufacturers asking what mixer handles dry starches, the answer is not a standard agitator alone. It is a properly configured vacuum emulsifying mixer or universal vacuum mixer processor with controlled powder induction, effective circulation, and sufficient shear for the formula.
The equipment choice matters because starch incorporation is a process problem as much as a mixing problem. The right system brings powder into the liquid quickly, disperses it before agglomerates develop, and maintains consistent conditions from the first bag to the final batch.
For mayonnaise, dressings, sauces, ketchup, and related viscous food products, a vacuum emulsifying mixer with a powder induction system is typically the strongest production solution. It combines vacuum-assisted powder charging with high-shear homogenization and low-speed scraping agitation in one sanitary processing platform.
Vacuum is especially valuable when handling fine, dry starches. Rather than allowing powder to fall through air and float across the vessel surface, the system uses negative pressure to draw it into the liquid phase. This reduces dust, limits operator exposure, and helps wet particles rapidly. The result is faster dispersion with fewer lumps and less rework.
A Universal Vacuum Mixer Processor can be the better fit when the production sequence includes more than powder incorporation. Many condiment formulas require blending, dispersion, emulsification, deaeration, heating or cooling, viscosity development, and final homogenization. A multi-function system keeps these steps controlled within one process environment, reducing transfers and giving the operator closer control over the batch.
The best mixer configuration depends on the starch type, addition rate, final viscosity, batch volume, and whether the formula requires a cooking or hydration stage. Equipment should be selected around the process, not around a generic horsepower rating.
A propeller, paddle, or simple sweep agitator can circulate liquid, but circulation alone does not guarantee powder wetting. Fine starch particles often sit on the liquid surface long enough to absorb moisture around their exterior. That exterior layer becomes sticky and forms a barrier around the dry powder inside. The familiar result is a soft or hard lump that persists through the batch.
Increasing agitator speed is not always the cure. Excessive surface turbulence can pull air into the product, create foam, and scatter powder around the vessel instead of drawing it below the surface. In emulsified products, entrained air can also affect density, appearance, filling accuracy, and product stability.
High shear is necessary, but it must be applied at the right point in the process. A rotor-stator homogenizer breaks down agglomerates and creates uniform dispersion, yet it performs best when the powder is already being fed into an active liquid stream. If operators add large quantities of starch directly into a stagnant or poorly circulating vessel, even a powerful homogenizer may spend valuable time chasing lumps instead of preventing them.
An effective dry-starch system combines powder induction, bulk movement, and localized high shear. Each function has a separate job, and all three must work together.
Vacuum powder induction creates a controlled route from the bag station or powder hopper into the processing vessel. The pressure differential pulls dry material toward the liquid instead of relying on gravity dumping. Operators can meter addition rates rather than introducing an entire bag at once.
This controlled addition is particularly useful for modified food starches, pregelatinized starches, gums, stabilizer blends, and dry ingredient premixes. These materials can hydrate quickly and are prone to lumping when rushed. Vacuum induction also supports cleaner production areas and more repeatable operator procedures.
An anchor agitator with wall and bottom scrapers moves the full mass of product, including material near the vessel jacket and corners. This matters as the batch thickens. In a high-viscosity dressing or sauce, a small high-shear head cannot provide enough vessel-wide movement by itself.
Scraping agitation promotes even temperature transfer when the formulation requires heating or cooling. It also prevents product buildup on heat-transfer surfaces, reducing localized overheating and supporting consistent hydration. For starch-thickened products, temperature uniformity is often as critical as mixing intensity.
The high-shear homogenizer provides the finishing force for dispersion and emulsification. In mayonnaise and creamy dressings, it helps reduce droplet size while breaking down powder agglomerates. In starch-containing sauces, it supports a smooth texture and a uniform viscosity profile.
The required shear level is formula-specific. Too little leaves graininess or incomplete dispersion. Too much can create unnecessary heat, alter sensitive ingredients, or change the desired texture. Process trials should establish the correct rotor-stator speed, recirculation pattern, and mixing time for each product family.
Not all starches behave the same way. Native starches commonly need a controlled heating cycle to gelatinize and develop viscosity. A mixer can disperse them effectively, but it cannot replace the correct time-temperature profile. If starch is added after the product has already thickened substantially, wetting becomes more difficult and processing time increases.
Pregelatinized and instant starches hydrate more quickly, which makes them useful for cold-process dressings and sauces. Their speed of hydration also raises the risk of fish eyes. These ingredients benefit from gradual vacuum induction into a well-circulating liquid phase, followed by a measured high-shear pass.
Modified starches vary widely. Some are selected for acid tolerance, freeze-thaw stability, clean flavor release, or resistance to process shear. A starch designed to retain body under severe processing may need different homogenizer settings than one intended for rapid cold swelling. Product developers and process engineers should review supplier guidance, then confirm the settings in pilot-scale trials before scaling to production.
Dry blends add another consideration. When starch is preblended with sugar, salt, gums, protein, spices, or acidulants, the mixer must accommodate the behavior of the complete blend. Sugar can improve powder flow in some cases, while gums can hydrate immediately and increase lumping risk. The system must be engineered for the hardest-to-disperse component, not the easiest one.
The most reliable process starts with the correct liquid phase, temperature, and agitation level before powder enters the vessel. Establish bulk circulation first. Then begin vacuum induction at a controlled rate while the homogenizer or recirculation loop is operating according to the validated recipe.
Avoid adding starch too quickly simply to shorten operator time. A slower, consistent feed rate often reduces total batch time because it prevents the need for extended mixing, screening, or rework. Once the powder is fully dispersed, continue the required hydration, heating, cooling, emulsification, or deaeration steps under controlled conditions.
For an oil-in-water emulsion such as mayonnaise or a creamy dressing, starch addition timing must also align with the emulsification sequence. Some formulas perform best when starch is hydrated in the aqueous phase before oil addition. Others require a specific addition point to manage viscosity and maintain pumpability. There is no single sequence for every formulation, which is why equipment and process design should be evaluated together.
A process that works in a laboratory blender may fail at 1,000 gallons. At production scale, powder feed distance, vessel geometry, recirculation flow, liquid level, viscosity, and heat-transfer area all affect results. Simply installing a larger motor does not reproduce pilot performance.
A production system should provide repeatable powder feed control, adequate vacuum capacity, a sanitary powder inlet arrangement, and agitation sized for the final product viscosity. It should also allow operators to run repeatable recipes with defined speeds, temperatures, vacuum levels, and hold times. These controls turn starch handling from an operator-dependent task into a stable manufacturing process.
PerMix designs vacuum emulsifying systems around these real production conditions, including difficult dry powders and demanding condiment formulations. The objective is direct: reduce lumping, protect emulsion quality, shorten avoidable processing time, and deliver a batch that performs the same way at commercial scale.
Before specifying a mixer, test the actual starch, liquid phase, process temperature, and target viscosity together. The right equipment is the one that gives your team controlled powder incorporation without sacrificing the texture, stability, and throughput your customers expect.
Get in touch with us today and learn how to we can help your business.