PerMix Mayonnaise Production
PerMix News
A sauce that looks smooth at the mixer can still separate in the warehouse, thin out after hot filling, or develop an inconsistent mouthfeel from batch to batch. Sauce homogenizers address the point where formulation and mechanical energy must work together: reducing droplets, dispersing powders, and building a stable structure that holds through processing, filling, and shelf life.
For commercial manufacturers, the objective is not simply high shear. The objective is repeatable product quality at the required throughput, with a process that operators can run reliably. The right homogenization system helps protect texture, appearance, viscosity, and emulsion stability while reducing rework and batch variability.
A homogenizer applies controlled mechanical shear to break down dispersed particles or droplets and distribute them more uniformly throughout a continuous phase. In mayonnaise and oil-based dressings, this commonly means reducing oil droplet size and producing a tighter droplet-size distribution. The result can be a smoother texture, improved visual uniformity, and a more stable emulsion.
In ketchup, barbecue sauce, cheese sauce, and starch-thickened products, the equipment may also be responsible for dispersing dry ingredients, breaking agglomerates, and integrating gums, stabilizers, tomato solids, spices, or other functional ingredients. These tasks are connected, but they are not identical. A system that creates an excellent oil-in-water emulsion may still struggle if powder addition is poorly controlled or if the batch has dead zones.
This is why homogenizer selection should begin with the formula and the process sequence, not a horsepower figure alone. Oil level, viscosity, particle content, temperature, batch volume, powder behavior, and fill method all affect the level and duration of shear required.
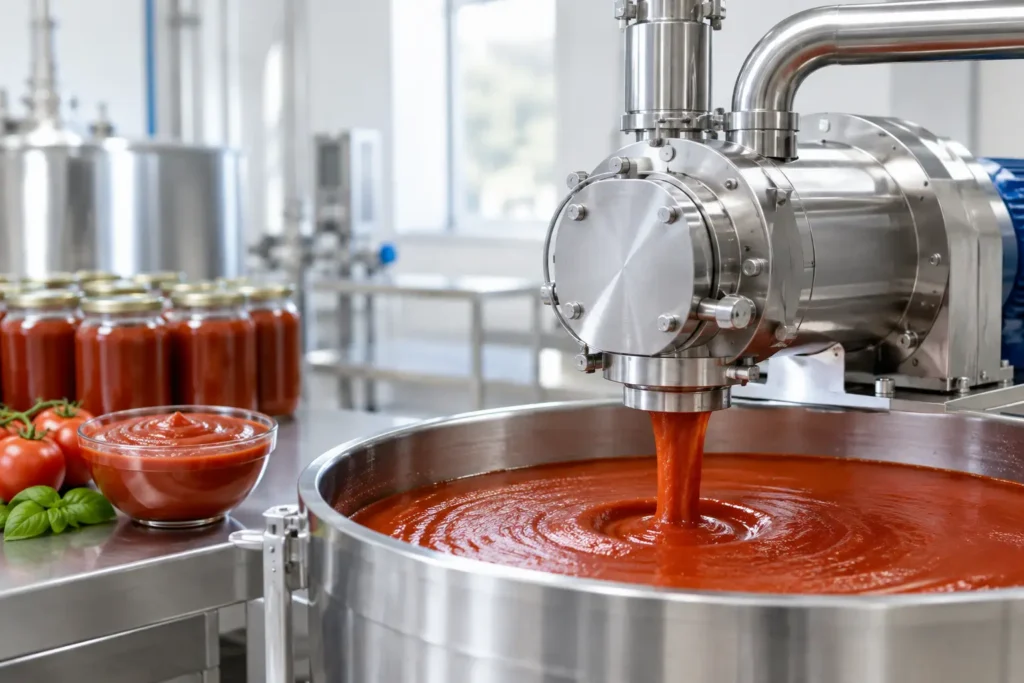
Conventional agitation moves product around the vessel. That circulation is necessary, especially in high-viscosity sauces, but it does not always create enough localized energy to fully disperse difficult ingredients or reduce oil droplets to the desired range. A rotor-stator homogenizer creates intense shear in a defined work zone, where product is accelerated through narrow openings and subjected to mechanical forces that break down droplets and agglomerates.
For mayonnaise, that action supports the emulsifier’s role in stabilizing oil droplets within the aqueous phase. For low-fat mayonnaise, fat-free products, and vegan formulations, the margin for error can become narrower. These recipes often rely more heavily on starches, hydrocolloids, proteins, or other texture-building systems. Inadequate dispersion can lead to fish eyes, lumps, weak body, poor gloss, or viscosity drift after hydration.
More shear is not automatically better. Excessive shear can damage a delicate texture, introduce unnecessary heat, or change the way a starch or hydrocolloid performs. The correct target depends on the formula. A pourable dressing may need a different droplet profile and viscosity than a spoonable mayonnaise or a particulate sauce with visible herbs and spices.
A fine emulsion often improves stability, but finished sauce performance depends on several factors at once. The emulsifier system must be suitable for the oil phase and processing conditions. Viscosity must be sufficient to control droplet movement. The pH, salt level, temperature, and order of addition must support the formula.
Homogenization cannot correct an incompatible formulation, but it can make a well-designed formula perform consistently. It also gives process teams a practical way to control variation when raw material properties shift between suppliers or seasonal lots.
Food manufacturers usually begin evaluating sauce homogenizers after a recurring production problem appears. A product may separate after storage. A low-fat dressing may lose body. Dry starch may form lumps during addition. One production line may deliver a different texture than another despite using the same recipe.
The underlying cause is often a combination of formulation, sequence, and equipment capability. A low-speed agitator may not provide the shear needed for fast wetting and dispersion. Adding powders directly into a full vessel can create floating rafts and agglomerates that are difficult to break later. Processing a viscous batch without effective circulation can leave portions of the vessel underworked.
Vacuum processing can be equally relevant. When air is entrained during high-speed mixing, it can create foam, affect density, dull product appearance, and complicate filling accuracy. Vacuum helps remove air from the batch while supporting a cleaner finished appearance and more controlled processing. This is particularly valuable for mayonnaise, creamy dressings, and dense sauces where trapped air is difficult to release naturally.
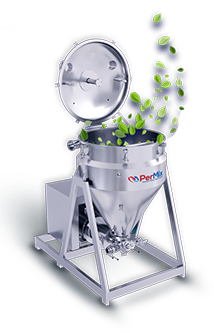
A properly designed vacuum emulsifying mixer combines vessel agitation, high-shear homogenization, and vacuum capability in one controlled process environment. It can reduce transfers between pieces of equipment, simplify cleaning, and give operators better control over the sequence from liquid charging through powder incorporation and final emulsification.
Batch homogenization is often the practical choice for manufacturers producing multiple SKUs, varying batch sizes, or formulations that require staged ingredient addition. The operator can hydrate gums, incorporate powders, build the water phase, add oil under controlled conditions, and apply high shear at defined points in the batch. This approach supports flexibility and is especially useful for mayonnaise, dressings, and specialty sauces.
Inline homogenization is well suited to continuous production or recirculation loops where high throughput and consistent processing are priorities. Product passes through a high-shear workhead as it moves through the system. It can be effective for final smoothing, recirculation-based emulsification, or controlled processing before downstream filling.
Neither approach is universally superior. A high-volume ketchup line may benefit from a continuous system, while a manufacturer making conventional, vegan, and low-fat mayonnaise on the same equipment may require the flexibility of a batch vacuum processor. The decision should account for annual volume, changeover frequency, product range, cleaning requirements, and future capacity plans.
The point of powder addition frequently determines whether a batch runs efficiently or becomes a rework event. Starches, gums, milk powders, proteins, and seasoning blends can agglomerate when they contact liquid too quickly or without sufficient wetting energy.
A powder induction system draws dry ingredients into the liquid stream under controlled conditions, helping achieve rapid wetting and dispersion. It reduces airborne dust, shortens manual addition time, and helps operators avoid the inconsistent results associated with dumping bags into an open vessel. For sauces with demanding dry-phase requirements, this capability can be as valuable as the homogenizer itself.
Equipment sizing starts with the finished product, not just the nominal vessel volume. A supplier should understand the minimum and maximum batch size, target viscosity, particulate content, oil percentage, processing temperature, and expected production schedule. These details determine the required motor power, rotor-stator configuration, agitator design, and recirculation strategy.
Sanitary construction also deserves close attention. Food-contact surfaces should be designed for thorough cleaning, with minimal areas where product can stagnate. The vessel geometry, bottom entry configuration, valve selection, and clean-in-place requirements all influence downtime and sanitation confidence. A system that homogenizes well but takes too long to clean can limit effective plant capacity.
Consider the process as a whole. If the sauce requires heating, cooling, vacuum deaeration, high-shear emulsification, and powder induction, separate machines may add complexity, transfer losses, and cleaning burden. An integrated processing platform can provide stronger control while keeping the production footprint manageable.
The best results come from treating homogenization as a defined processing step rather than a correction applied at the end of the batch. Document the order of addition, temperature window, vacuum level, homogenizer speed, run time, and agitation setting for each formula. Then verify finished-product performance through viscosity checks, visual inspection, density measurements, and shelf-life testing.
This discipline becomes more valuable as production scales. A pilot batch may tolerate small variations that become costly at industrial volume. When the process is controlled, R&D teams can move from formulation trials to repeatable commercial production with fewer surprises.
For manufacturers producing mayonnaise, dressings, and demanding viscous sauces, PerMix designs vacuum emulsifying systems around the full production challenge: efficient powder incorporation, controlled high shear, dependable vacuum performance, and scalable batch consistency. The right system should make difficult sauces easier to manufacture, not simply mix them faster.
A reliable sauce process is built when the equipment, formulation, and operating method are matched from the first ingredient charge. That is where stable texture, clean production runs, and confidence at scale begin.
Get in touch with us today and learn how to we can help your business.