PerMix Mayonnaise Production
PerMix News
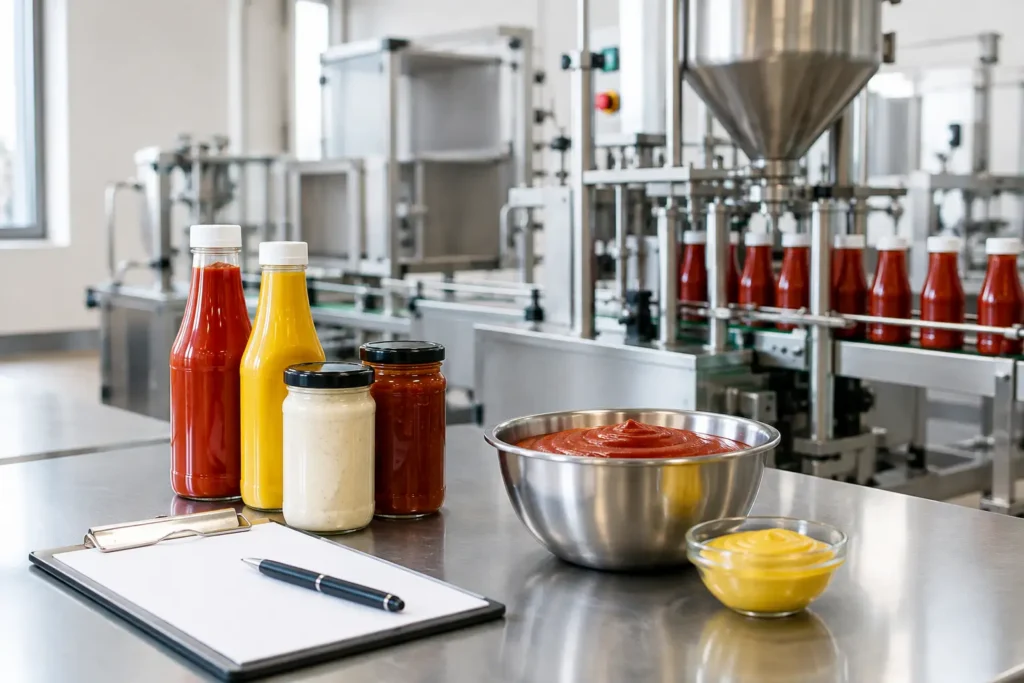
A mayonnaise line can look complete on a layout drawing and still fail at the moment dry starch forms fish eyes, oil is added too quickly, or a finished emulsion will not transfer cleanly to the filler. A practical condiment manufacturing equipment checklist starts with the product behavior, not a generic list of tanks. The right system must disperse powders, form and protect the emulsion, maintain sanitation, and repeat the same result across every commercial batch.
For mayonnaise, dressings, ketchup, sauces, and similar viscous products, equipment selection is a process decision with a direct effect on texture, stability, yield, labor, and line uptime.
Before specifying a mixer or requesting a quotation, define what the process must achieve. A conventional full-fat mayonnaise, a low-fat dressing, and a vegan mayonnaise may use similar production stages, but they do not place the same demands on shear, vacuum, powder handling, or batch time.
Document the target batch size, annual volume, shifts, expected future capacity, and the number of SKUs to be produced. Include viscosity ranges, particle-size expectations, oil phase percentage, acid addition point, heat-sensitive ingredients, and any particulates that must remain intact. This information determines whether a simple batch vessel is sufficient or whether the plant needs an integrated vacuum emulsifying process.
Also identify the real operating constraint. Some plants need faster batch turnover. Others need better emulsion stability, easier cleaning between allergen-containing formulas, or controlled powder charging without airborne dust. The equipment should be sized around that constraint, not only around gallons per batch.
A complete system does not require every item in every facility. The checklist below helps separate essential process equipment from options that add value only when the formulation or production plan justifies them.
Liquid oil, vinegar, water, liquid egg, sweeteners, and other bulk ingredients need storage and transfer equipment that preserves quality and supports repeatable batching. Specify compatible tanks, sanitary pumps, filtration where appropriate, level indication, and transfer lines designed for the product viscosity.
For dry ingredients, assess how powders will be received, stored, weighed, and delivered. Starches, gums, salt, sugar, mustard powder, proteins, and stabilizers can become a major source of variability when operators manually add bags to an open vessel. A controlled handling arrangement reduces dust, improves traceability, and supports more consistent addition rates.
The main processing vessel must be selected for more than nominal capacity. Evaluate usable working volume, vessel geometry, jacket requirements, sanitary design, and agitation coverage at both minimum and maximum batch levels.
For viscous condiments, an anchor agitator with wall scraping is often necessary to prevent product buildup, improve heat transfer, and keep the batch moving uniformly. A vessel that performs acceptably with a thin sauce may leave dead zones when processing a heavy mayonnaise or high-solids ketchup.
Ask how the agitator handles viscosity changes during the batch. Many formulas begin as a low-viscosity water phase and become substantially thicker after oil addition, hydration, or cooling. Drive torque and speed control must accommodate the finished product, not just the starting liquid.
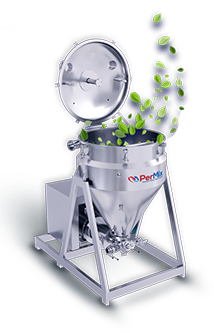
This is the core equipment decision for emulsified condiments. A high-shear rotor-stator homogenizer reduces droplet size, disperses functional ingredients, and builds the smooth, stable structure expected in commercial mayonnaise and dressings.
The required shear level depends on the formulation. High-oil mayonnaise typically demands reliable emulsion formation and controlled oil incorporation. Low-fat and fat-free formulas can be more sensitive because starches, gums, proteins, and water-phase ingredients must provide body that oil would otherwise supply. Vegan products may require precise dispersion of plant proteins and hydrocolloids while avoiding conditions that destabilize the system.
Compare the homogenizer’s actual process placement and recirculation path, not only its motor horsepower. An inline unit may suit a continuous or recirculated process, while an integrated bottom-entry emulsifier can provide efficient processing in a vacuum vessel. The best configuration depends on batch size, viscosity, formulation sensitivity, and desired cycle time.
Vacuum processing is often a performance requirement rather than a luxury. It helps remove entrained air, improves the appearance of the finished condiment, supports stable emulsification, and can assist with drawing powders into the batch.
Air removal matters when the product must have a dense, glossy appearance and reliable filling weights. Excess air can contribute to oxidation risk, inconsistent density, foaming, and unstable product behavior during downstream filling. For products requiring powder induction, vacuum can also support cleaner, more controlled ingredient addition.
Specify vacuum level, pump type, condensate handling, and the control method used to maintain vacuum during processing. The system must be designed for food production and for the actual vapor load created by the process.
Powder addition is one of the most common failure points in condiment production. A mixer can create high shear and still struggle if dry ingredients are dumped too quickly, poorly wetted, or added in the wrong sequence.
A powder induction system should draw ingredients into a high-energy zone where they wet out rapidly and disperse before agglomerates form. This is especially valuable for starches, gums, milk powders, proteins, and stabilizer blends. It can reduce operator exposure, shorten batch times, and improve formula repeatability.
Verify the system’s ability to handle your specific powders. Free-flowing sugar behaves very differently from fine xanthan gum or pregelatinized starch. Test difficult ingredients whenever possible, particularly if the line must produce low-fat, fat-free, or vegan formulations.
Many condiments require temperature control for hydration, pasteurization, viscosity development, or cooling before filling. Confirm whether the vessel jacket, heat exchanger, or both can reach required temperatures within the available cycle time.
Heating capacity should be matched to the batch mass, starting temperature, utility conditions, and product thermal sensitivity. Cooling deserves equal attention. Slow cooling can delay filling, reduce daily output, and create unnecessary time in the processing vessel.
For formulations containing eggs or other temperature-sensitive ingredients, the process must be engineered around food safety requirements and ingredient handling limits. A high-performing mixer cannot correct a poorly defined thermal process.
The finished condiment must leave the mixer without losing the texture created during processing. Choose transfer pumps that handle product viscosity without excessive shear, pulsation, or air introduction. Progressive cavity, lobe, twin-screw, and other sanitary pump designs each have different strengths.
Consider whether a buffer tank is necessary between processing and filling. It can keep the filler supplied and reduce downtime, but it also adds a cleaning step and can expose product to longer hold times. For shorter runs or highly sensitive emulsions, direct transfer may be the better choice.
Confirm that the process system and filler communicate effectively on flow, level, and start-stop conditions. An undersized transfer path can turn a high-capacity mixing system into a bottleneck.
Controls determine whether the process is repeatable from one operator and shift to the next. At minimum, the system should provide clear control of agitation speed, homogenizer speed, temperature, vacuum, ingredient addition, and timing.
For larger plants or tightly controlled formulas, recipe management and batch data capture provide greater value. Automated sequencing can enforce the correct addition order, record critical process values, and reduce dependence on manual judgment. The appropriate level of automation depends on SKU complexity, staffing, regulatory needs, and the cost of a rejected batch.
Condiment equipment must be cleanable by design, not by operator effort. Review weld quality, internal surface finish, drainability, gasket materials, spray device coverage, valve selection, and access to components that contact product.
A clean-in-place system is particularly valuable for plants running multiple products or managing allergen changeovers. However, CIP performance depends on properly designed piping circuits, chemical concentration, flow velocity, temperature, and verification practices. Do not assume that adding a CIP skid solves cleaning challenges in a process line with poor drainage or dead legs.
A strong supplier should be able to discuss more than vessel size and price. Ask for expected batch times, utility requirements, product-contact materials, cleaning approach, controls scope, and the operating range for viscosity and batch volume. Request clarity on how the system handles your most difficult powder, highest-viscosity formula, and lowest-volume batch.
It is also wise to evaluate service access, spare parts, lead time, commissioning support, warranty coverage, and operator training. The lowest initial equipment price can become expensive when production delays, poor sanitation access, or inconsistent emulsions consume labor and product.
PerMix designs mayonnaise production systems around these process realities, including vacuum emulsification and powder induction for demanding condiment formulations. The goal is not simply to install a mixer. It is to build a process that produces the intended texture, stability, and output every day.
Use this checklist during formulation scale-up and again before final equipment approval. The best line is the one that gives your operators control over the difficult moments in the batch, when powder must disperse, an emulsion must hold, and production cannot wait.
Get in touch with us today and learn how to we can help your business.