PerMix Mayonnaise Production
PerMix News
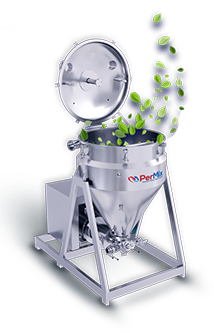
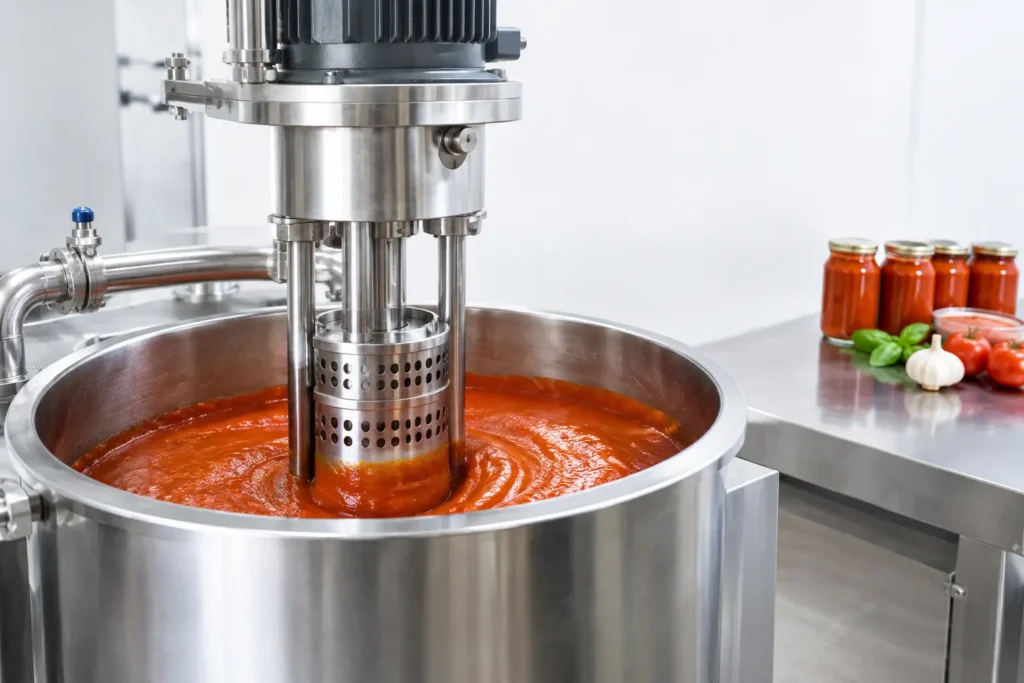
A vacuum homogenizer performance review should start where production losses start: at the batch. If mayonnaise separates after filling, a low-fat dressing feels thin, or dry starch forms stubborn fisheyes, the issue is rarely just the recipe. It is the combined effect of shear, vacuum, powder wetting, thermal control, vessel geometry, and operating discipline.
For commercial sauce manufacturers, a vacuum homogenizer is not simply a mixer with a lid. It is a process system that determines whether a formulation moves reliably from R&D to repeatable, saleable production. The strongest machines do more than create an attractive emulsion in one trial. They maintain texture, appearance, viscosity, and stability across shifts, operators, and batch sizes.
Performance is best judged against the product and the production target, not against motor horsepower alone. A high-oil mayonnaise, an egg-free vegan mayonnaise, and a fat-free dressing can all require different process conditions. The equipment must provide enough flexibility to handle that range without sacrificing control.
The first benchmark is emulsion quality. A properly selected homogenizing system reduces dispersed-phase droplet size and distributes ingredients uniformly through the batch. In mayonnaise and dressings, this directly affects gloss, body, mouthfeel, and resistance to oil separation. A machine may produce a smooth-looking product at discharge, yet still underperform if the emulsion loses structure during storage or after temperature cycling.
The second benchmark is repeatability. A production line cannot depend on a highly experienced operator making adjustments by feel. Variable-speed agitation, controllable homogenizer speed, managed ingredient addition, and a stable vacuum profile give the processor defined operating windows. That means less variation between batches and faster training for production teams.
Throughput matters, but it should be measured honestly. Fast batch time is valuable only when it includes charging, powder incorporation, emulsification, deaeration, discharge, and cleaning. A mixer that reaches target viscosity quickly but requires extended cleanup or frequent rework is not delivering real capacity.
A meaningful equipment review should examine actual product trials and operating data. Water-only demonstrations, while useful for checking basic functions, do not show how a system manages oil, gums, starches, proteins, acids, and high-viscosity phases.
The homogenizer is the heart of the system, but its performance depends on how material reaches the rotor-stator zone. Effective circulation exposes the entire batch to controlled high shear rather than overprocessing material nearest the homogenizer.
For a standard mayonnaise, look for a uniform, stable emulsion with no visible oiling-off and a consistent texture from the top to the bottom of the vessel. For low-fat and fat-free products, assess whether the system can fully hydrate stabilizers and develop body without excessive processing time. For vegan formulations, confirm that plant proteins, starches, and hydrocolloids disperse cleanly while the finished product retains the intended creamy profile.
More shear is not automatically better. Excessive shear can affect viscosity development, create unwanted heat, or damage sensitive ingredients. The right system provides the range to apply high energy when needed and reduce intensity once the target structure is achieved.
Powder handling is often where a batch either becomes efficient or becomes expensive. Dry starches, gums, milk powders, salt, sugar, and functional ingredients can clump when added directly into a viscous liquid. Once agglomerates form, extra mixing time may not fully correct the problem.
A well-designed vacuum processing system uses vacuum draw and controlled powder induction to pull ingredients into the batch quickly and wet them thoroughly. This can reduce airborne dust, shorten addition time, and prevent fisheyes before they enter the product.
Review the powder system using the hardest ingredient in the formula, not the easiest. If the process can consistently incorporate starch or hydrocolloids at the required rate without lumping, it is far more likely to handle routine ingredients efficiently. The test should also confirm that powder addition does not overload the homogenizer or create dead zones in the vessel.
Vacuum serves several production purposes. It helps remove entrained air, supports powder induction, and can improve product appearance and filling behavior. Air in mayonnaise or dressings can produce a lighter-than-intended appearance, inaccurate fill weights, oxidation risk, and unstable viscosity readings.
The best vacuum result is not necessarily the deepest vacuum at every stage. Product temperature, volatility, ingredient behavior, and batch sequence all matter. Strong vacuum during powder addition may improve wetting, while controlled deaeration after emulsification can help achieve a denser, more uniform finished product. A processor should allow operators to manage these stages rather than treat vacuum as a fixed setting.
Many emulsified sauces require temperature management for hydration, pasteurization steps, viscosity control, or cooling before filling. The vessel jacket, heat-transfer area, product movement, and control logic all influence performance.
Evaluate heating and cooling with a loaded batch. A system may show acceptable jacket temperatures while still heating unevenly if product circulation is weak. The same concern applies during cooling, especially with high-viscosity formulations. Slow cooling holds product in the vessel longer, extends the batch cycle, and can become a bottleneck when demand increases.
A few gallons left in a vessel or transfer line may seem minor until it is multiplied across multiple batches and high-value ingredients. Efficient discharge supports yield, while properly positioned valves and sanitary piping reduce trapped product and simplify cleaning.
Clean-in-place capability, accessible seals, sanitary weld quality, and suitable surface finish deserve close attention. Food manufacturers should ask how long cleaning takes between compatible products and what changes when moving from an egg-based mayonnaise to an allergen-sensitive or vegan line. The right answer depends on the plant’s sanitation program, but equipment design should make compliance practical rather than labor-intensive.
A pilot batch can perform well and still fail during scale-up. Larger vessels change liquid height, circulation paths, heat-transfer behavior, and powder-addition dynamics. Selecting equipment only by total vessel volume is a common mistake.
Useful working volume, minimum batch size, viscosity range, ingredient addition rate, and downstream filling requirements should guide sizing. A manufacturer producing several sauce families may need a flexible processor with variable-speed mixing and configurable powder handling. A plant focused on high-volume classic mayonnaise may prioritize repeatable cycle time and rapid turnaround.
Control systems also become more valuable as production expands. Recipe management, repeatable speed settings, temperature control, vacuum sequencing, and batch records help protect quality when production is transferred between operators or facilities. Automation should support the process, not hide it. Operators still need clear visibility into what the batch is doing and why.
Equipment price is only one part of the investment. The more useful calculation is cost per good batch over the system’s working life. Consider rework, product loss, labor during powder addition, utility use, cleaning time, maintenance access, and the cost of inconsistent quality reaching the market.
A lower-cost machine may be appropriate for a simple, low-viscosity sauce with limited production demands. However, when a line must handle difficult powders, multiple formulations, high oil loads, or strict consistency requirements, under-specifying the process system can cost far more than the initial savings.
PerMix evaluates vacuum emulsifying mixers around real processing demands, including mayonnaise, ketchup, dressings, and adjacent viscous products. The right configuration begins with the formula, batch target, ingredient challenges, and required production rhythm.
Before approving a system, run a representative product trial, define measurable acceptance criteria, and review the full batch cycle with your operations team. A vacuum homogenizer earns its value when it gives production the confidence to make the same product right again tomorrow – at the speed, yield, and quality your market requires.
Get in touch with us today and learn how to we can help your business.