PerMix Mayonnaise Production
PerMix News

A mayonnaise line rarely loses time in one obvious place. The delay is usually distributed across powder wet-out, oil addition, vacuum pull-down, viscosity development, transfer, and cleanup. Effective mayonnaise batch time reduction addresses the complete process, not just mixer speed. The objective is to produce more saleable batches per shift while protecting emulsion stability, texture, flavor distribution, and sanitary control.
For commercial producers, a shorter batch is only valuable when it remains repeatable. A system that reaches target viscosity quickly but introduces air, leaves starch fisheyes, or produces a weak emulsion simply shifts the cost to rework, hold time, or product loss. The right improvement strategy removes nonproductive time while maintaining tight control over the critical steps of emulsification.
Batch records often show a respectable mixing time but conceal long delays before and after mixing. Operators may spend excessive time charging ingredients, waiting for powders to hydrate, correcting viscosity, recovering vacuum, or flushing product from lines. These stages should be measured separately before equipment changes are specified.
The largest opportunity is frequently powder incorporation. Egg powders, modified starches, gums, salt, sugar, acids, stabilizers, and protein-based vegan ingredients can bridge, float, agglomerate, or hydrate unevenly when introduced through an open vessel. Operators then extend the batch to break down visible particles or compensate for incomplete dispersion. More mixer time is not always the answer. Controlled powder induction is usually faster and more reliable than prolonged high-speed agitation.
Oil addition is another common constraint. Adding oil too aggressively can overload the emulsion, particularly with lower-fat formulas or products using alternative proteins. Adding it too slowly protects the emulsion but consumes capacity. The practical target is a controlled addition rate that matches the emulsifying capability of the rotor-stator system and the formulation’s available emulsifier.
Cleanup and changeover deserve equal attention. A fast processing vessel that requires extended manual cleaning or difficult disassembly may not improve total plant output. For plants running multiple mayonnaise, dressing, or sauce SKUs, clean-in-place design, low product hold-up, and predictable wash cycles are production assets.
Before selecting a larger or faster mixer, map the current batch from first ingredient charge through vessel release. Record the time required for liquid charging, powder addition, hydration, oil dosing, homogenization, vacuum operation, final adjustment, discharge, and cleaning. Include waiting time, not only active operating time.
This analysis reveals whether the bottleneck is mechanical, procedural, or formulation-driven. A batch that spends 20 minutes waiting for an operator to manually add dry ingredients has a different solution than a batch that requires 20 minutes of additional homogenization to reach a smooth texture.
It also prevents a common capital mistake: buying a larger vessel when the real limitation is slow ingredient handling or downstream filling capacity. A correctly sized system must support the desired batch volume, but it must also reduce the slowest stage in the full production cycle.
Time targets should be established alongside product specifications. Define acceptable viscosity range, particle-free appearance, emulsion stability, finished temperature, pH, density, and sensory texture. For high-oil conventional mayonnaise, droplet size and emulsion strength are central concerns. For low-fat, fat-free, and vegan mayonnaise, powder hydration, starch activation, protein functionality, and body development may become more demanding.
This is where process trials matter. A reduction that works on a standard mayonnaise formula may not transfer directly to an egg-free product containing pea protein, starch, or hydrocolloids. The production system needs enough flexibility to manage both recipes without forcing operators to use excessively long cycle times as a safety margin.
Vacuum emulsification supports batch efficiency in several ways. By processing under vacuum, manufacturers can reduce entrapped air, improve product density, and achieve a cleaner visual appearance. Less air also helps prevent false volume readings and can support more consistent filling performance downstream.
Vacuum can improve ingredient incorporation when used with an appropriately designed induction arrangement. Powders can be drawn into the liquid phase under controlled conditions rather than being dumped into the vessel surface. This reduces airborne dust, minimizes operator intervention, and helps prevent dry pockets that require extended mixing.
Vacuum is not a substitute for correct process sequence. Pulling high vacuum too early can interfere with charging or create undesirable foaming in certain formulations. The best operating profile depends on the recipe, vessel geometry, powder characteristics, and temperature. Automation should allow recipes to define when vacuum is applied, at what level, and for how long.
Powder handling is often the fastest path to meaningful throughput gains. A high-performance induction system creates immediate contact between powders and the liquid stream, then recirculates the material through a high-shear zone for rapid dispersion. This is particularly valuable for difficult dry starches and fine hydrocolloids that tend to form gels on contact with water.
The key is to avoid treating all powders the same way. Salt and sugar may dissolve quickly, while starches and gums require controlled addition rates and specific shear conditions. Premixing every dry ingredient can simplify operator handling, but it can also make flow behavior less predictable. Individual feeding or grouped additions may deliver better consistency for complex recipes.
Temperature should be controlled as part of this stage. Excessive shear can add heat, and some ingredients respond poorly when hydrated outside a narrow temperature range. Faster processing is only productive when it does not create a cooling delay before discharge or damage the finished product structure.
A mayonnaise emulsification system must create fine, stable oil droplets without overprocessing the product. Rotor-stator shear, recirculation flow, and oil addition rate work as one process. Increasing one variable without considering the others can cause instability or unnecessary energy use.
For a conventional full-fat mayonnaise, a well-designed high-shear emulsification zone can support a faster oil addition profile once the aqueous phase is properly prepared. For low-fat mayonnaise, the process may require more attention to starch and stabilizer hydration before oil is introduced. Vegan mayonnaise can require additional control because plant proteins may respond differently to pH, salt, shear, and temperature than egg-based emulsifiers.
Automation makes this control repeatable. Recipe-driven control of agitation speed, homogenizer speed, vacuum level, ingredient timing, oil flow, and processing duration removes dependence on individual operator judgment. It also gives process engineers usable data when a formula or raw material changes.
A production system should be evaluated by shift output, not only its mixing performance. Fast discharge, minimal residual product, sanitary valve design, and efficient clean-in-place coverage can determine whether the plant gains an additional batch each day.
Transfer design matters here. Long pipe runs, dead legs, undersized pumps, and high-viscosity product left in lines add time and reduce yield. The discharge system should be selected for the finished mayonnaise viscosity and the distance to the filler or buffer tank. A vessel that empties quickly but leaves significant product behind is not delivering the expected economic return.
For facilities with frequent SKU changes, organize campaigns where practical. Running compatible formulas in sequence can reduce cleaning intensity and setup time. However, allergen management, label claims, and customer requirements must always take priority over scheduling convenience.
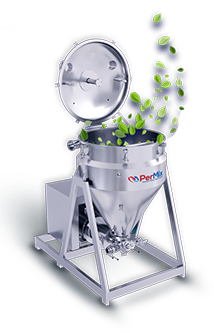
The most effective solution combines vessel design, vacuum capability, powder induction, high-shear emulsification, automated controls, and sanitary construction. PerMix vacuum emulsifying mixers are engineered around this complete production requirement, helping manufacturers shorten processing cycles while maintaining the stable, smooth mayonnaise their customers expect.
Equipment sizing should account for working volume rather than nominal vessel volume alone. It should also consider recipe viscosity, powder load, desired batch frequency, future product extensions, utilities, cleaning requirements, and downstream capacity. An oversized system can create poor small-batch performance, while an undersized unit can force operators to run conservative, time-consuming cycles.
The most reliable path forward is a structured production trial using your actual formula, raw materials, and quality targets. Measure each stage, confirm the finished emulsion, and calculate throughput based on the complete batch-to-batch cycle. When the process is engineered around the real bottleneck, faster mayonnaise production becomes a repeatable operating standard rather than a one-shift improvement.
Get in touch with us today and learn how to we can help your business.