PerMix Mayonnaise Production
PerMix News
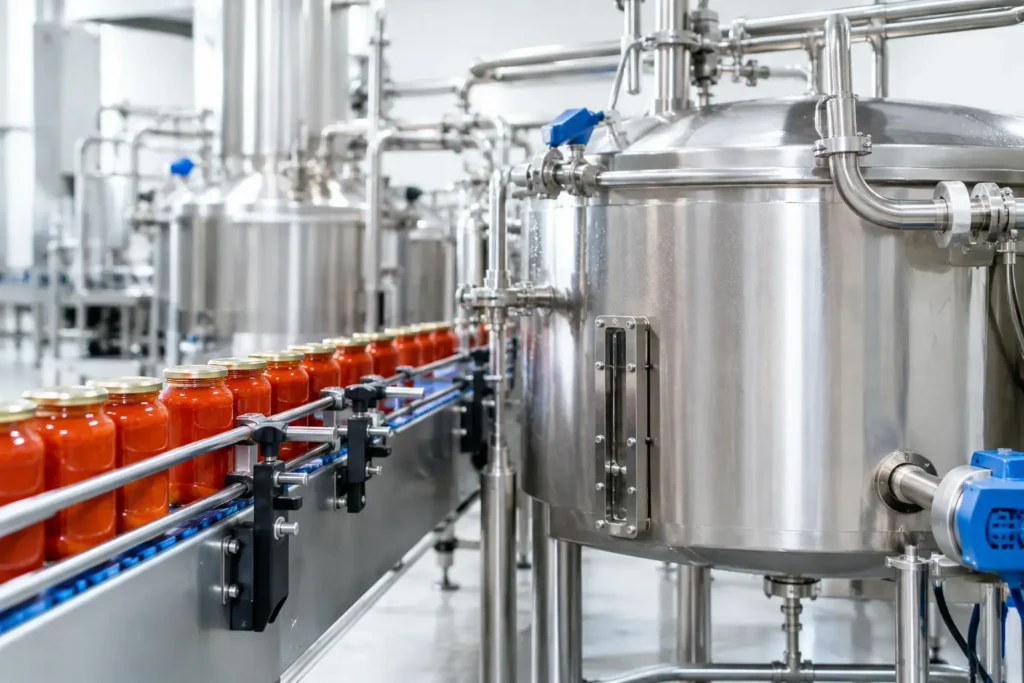
A sauce line can produce a clean-looking batch and still leave behind the residues that create the next production problem. Oil films, starch deposits, protein soils, gums, and trapped product in valves or recirculation paths do not respond to the same cleaning sequence. The best CIP practices for sauce production are built around the actual product, the equipment geometry, and verified results – not a fixed cycle copied from another process.
For mayonnaise, dressings, ketchup, and similar viscous products, cleaning-in-place is a production discipline. A well-designed CIP program protects food safety, limits allergen carryover, reduces unplanned downtime, and keeps emulsifying equipment ready to deliver consistent texture from batch to batch.
Every effective CIP cycle begins with a clear understanding of what must be removed. A high-oil mayonnaise leaves a very different soil profile than a tomato ketchup, a starch-thickened barbecue sauce, or a vegan dressing formulated with plant proteins and hydrocolloids.
Fat-rich emulsions can coat vessel walls, pipelines, transfer pumps, homogenizer heads, and valve seats with persistent oil films. These films can shield other residues from the cleaning solution. Starch systems may gel or bake onto heat-transfer surfaces. Tomato-based sauces introduce pigment, sugar, acid, and burnt-on residues where thermal processing is involved. Protein-containing products may require more focused alkaline cleaning, especially after elevated-temperature processing.
This is why one cleaning recipe rarely performs equally well across every SKU. Plants running multiple sauce families should establish validated cycles by product category, then define when a longer or more intensive cycle is required. The goal is not to run the harshest cycle every time. The goal is to remove the soil completely with the least practical use of water, energy, time, and chemicals.
A CIP system cleans by delivering the right chemistry, temperature, mechanical action, and contact time to every product-contact surface. If one of these factors is weak, the cycle may look complete on the control screen while residues remain in the system.
Mechanical action is often the limiting factor in viscous sauce operations. Cleaning solution must reach sufficient velocity through pipelines to create turbulence and sweep away soil. Dead legs, oversized lines, poorly drained branches, partially opened valves, and incorrectly selected spray devices all reduce cleaning performance.
For vessels, verify that spray balls or rotary spray devices deliver complete wetting coverage at the specified flow rate and pressure. A spray device that is undersupplied can leave shadow areas under agitators, around manways, behind baffles, and near the vessel cone. These are common locations for dried emulsion, powder buildup, and microbial risk.
For recirculation loops, confirm flow at the point of use rather than relying only on pump capacity. Pipe diameter, elevation, backpressure, heat exchangers, valve clusters, and fouling all affect actual velocity. Flow meters, pressure monitoring, and return-line conductivity provide far more useful evidence than assumptions based on a pump curve.
Cleanability begins before the first CIP cycle. Sauce processing equipment should be designed with smooth product-contact surfaces, hygienic welds, correctly sloped lines, fully drainable vessels, and valve arrangements that isolate and clean every path.
Vacuum emulsifying mixers require particular attention. Product can remain beneath the agitator, within the emulsifying head, around shaft seals, and in powder induction circuits if those areas are not included in the cleaning path. The same applies to transfer hoses, inline filters, sampling valves, and balance tanks. Any component that contacts sauce must either be cleaned in place with verified coverage or removed under a controlled sanitation procedure.
A system designed for cleanability reduces the temptation to rely on manual rework after every cycle. That saves labor, but more significantly, it makes sanitation repeatable.
The sequence should fit the formulation and process conditions, but most sauce operations benefit from a disciplined progression: product recovery, initial rinse, alkaline wash, intermediate rinse, acid wash when needed, final rinse, and sanitation where the process requires it.
Product recovery should come first. Push or drain as much sauce from the line as possible before introducing water. This reduces chemical demand, lowers wastewater loading, and avoids sending recoverable product directly to the drain. For high-value emulsions, the economics can justify careful recovery design.
The initial rinse removes bulk residue and prepares the system for chemistry. Water that is too hot can set protein soils or thicken certain starch residues. Water that is too cool may leave fats attached to surfaces. The correct rinse temperature depends on the formula, so it should be established during validation rather than selected by habit.
An alkaline wash is commonly the main cleaning step for oil, protein, and many organic soils. Concentration and temperature must remain within the validated range for the full cycle. A caustic wash that starts at target strength but becomes diluted through poor rinse separation will not deliver predictable results.
Acid washing is not always necessary after every batch. It is useful when mineral deposits, hard-water scale, or process-related inorganic films are present. Overusing acid adds cost and can increase wear on seals and incompatible materials. Use it based on water quality, equipment condition, and verification data.
The final rinse should continue until return conductivity confirms that cleaning chemicals have been removed. If sanitizer is used, apply it at the correct concentration and contact time, then follow the plant’s validated drain or rinse procedure.
A CIP skid can automate a sequence, but it cannot compensate for missing control. Plants should continuously measure the conditions that determine cleaning performance: time, temperature, chemical concentration, flow, pressure, and return conditions.
Conductivity is especially valuable because it helps distinguish rinse water from chemical solution and confirms chemical recovery. However, conductivity alone does not prove that a surface is clean. It must be paired with flow records, temperature records, visual inspection at defined access points, and microbiological or allergen verification where applicable.
Temperature deserves close attention in sauce plants. Heat loss across long runs, jacketed vessels, and external equipment can pull the solution below its effective range before it reaches the dirtiest area. Conversely, excessive temperature can damage seals, affect gaskets, or bake residues onto heat-transfer surfaces. Use sensors at both supply and return locations when the system is complex enough to justify them.
Chemical concentration must also account for water hardness and soil load. Hard water can reduce detergent effectiveness and accelerate scale formation. High product carryover can exhaust cleaning chemistry sooner than expected. Titration checks and routine chemical management are practical safeguards, particularly on multi-shift lines.
Cleaning expectations rise sharply when one sauce contains egg, milk, soy, mustard, sesame, or other allergens and the next product does not. A standard visual check is not enough for allergen control. The cleaning procedure needs defined validation, documented verification frequency, and clear release criteria before the next run starts.
Changeovers also deserve extra scrutiny when moving from dark, strongly pigmented sauces to light-colored dressings, or from garlic, chili, smoke, and spice-heavy products to milder formulations. Flavor and color carryover can create customer complaints even when the product is microbiologically safe.
In many plants, the best answer is not simply a longer cycle. It may be dedicated hoses, a revised valve matrix, improved product recovery, a separate transfer route, or a production schedule that groups compatible products. Scheduling and sanitary design can reduce cleaning risk more effectively than adding ten minutes of caustic circulation.
A bright stainless-steel surface can still contain residues. Effective verification combines several methods: pre-operational inspection, ATP testing where appropriate, allergen swabbing, microbiological environmental monitoring, and periodic disassembly of high-risk components.
ATP testing provides a fast operational signal, but it should not be treated as a universal pass-fail answer. Some residues may produce weak signals, while chemical residues can interfere with results. Allergen-specific testing and microbiological testing should be selected according to the hazard being controlled.
Trend the results. A single failed swab requires action, but repeated marginal results around the same valve cluster, emulsifying head, or transfer loop point to a design or process issue. That data should drive corrective action, whether it is a changed CIP parameter, a gasket replacement, a spray-device upgrade, or a revised equipment configuration.
The strongest sauce manufacturers do not view CIP as downtime between profitable batches. They treat it as a controlled process that protects throughput, quality, and brand reputation. Shortening a cycle without validation can create expensive failures. Running an unnecessarily long cycle wastes capacity and utilities. The right balance comes from measured data and equipment designed to clean as effectively as it processes.
For sauce lines handling demanding emulsions, powders, and viscous formulations, PerMix vacuum mixing and emulsifying systems can be specified with process flow and sanitary access in mind. The practical objective is simple: produce the intended texture, recover more product, clean every critical surface, and start the next batch with confidence.
A CIP program earns its value when operators can trust the record, quality teams can trust the verification, and production can move to the next sauce without carrying yesterday’s batch into tomorrow’s label.
Get in touch with us today and learn how to we can help your business.