PerMix Mayonnaise Production
PerMix News
A mixer can produce a smooth mayonnaise batch and still create a sanitation problem that costs hours of downtime, wastes product, or puts a release schedule at risk. For condiment manufacturers, a sanitary mixer design guide must address more than polished stainless steel. The real question is whether every product-contact surface can be cleaned, inspected, drained, and returned to service without compromising emulsion quality.
Mayonnaise, dressings, ketchup, and similar products create a demanding design case. They can be viscous, sticky, oil-rich, powder-intensive, and difficult to remove from dead zones. A properly specified sanitary mixing system protects product quality while reducing the labor, water, chemicals, and production interruptions associated with cleaning.
Sanitary design begins with the actual formulation, not with a generic equipment specification. A thin vinaigrette, a high-viscosity mayonnaise, and a vegan emulsion may all require different mixing energy, recirculation rates, powder induction methods, and cleaning cycles. Those process decisions directly affect the vessel geometry and internal components that must be cleaned.
First, define whether the system will be cleaned in place, cleaned out of place, or opened for manual cleaning. Commercial mayonnaise production typically benefits from a validated clean-in-place, or CIP, strategy because frequent manual disassembly is slow and introduces operator variation. CIP is not simply a spray device mounted in a tank. It requires sufficient flow, chemical concentration, temperature, contact time, and coverage across the complete product path.
The cleaning method should also account for changeovers. A plant making egg-based mayonnaise and vegan mayonnaise, for example, may need a more demanding allergen-cleaning protocol than a single-product line. If low-fat and fat-free formulas use starches, gums, or protein systems that adhere to surfaces, cleaning performance must be verified against those residues rather than against water-soluble ingredients alone.
A sanitary vessel needs more than a smooth internal finish. Its shape must prevent product and cleaning solution from collecting in areas that cannot be effectively reached or drained. Product hold-up is not only a yield issue. Residual material can support microbial growth, contaminate the next batch, and make cleaning verification unreliable.
Specify a vessel bottom that drains to the lowest practical point, with an outlet sized for the product viscosity and production rate. Flat-bottom tanks can retain material unless the outlet and agitator arrangement are engineered carefully. Conical or dished bottom sections often improve drainage, but the best configuration depends on whether the system uses bottom-entry homogenization, a recirculation loop, or both.
Internal corners should use generous radii rather than sharp transitions. Welds must be continuous, smooth, and finished to prevent crevices where mayonnaise, starch, or seasoning particles can lodge. Avoid internal brackets, exposed threads, unnecessary gussets, and structural features that create shadow areas for CIP spray.
Vessel sizing also matters. An oversized tank may leave a low-level batch below the effective operating range of the agitator or homogenizer. An undersized tank can cause vortexing, foam, poor powder wetting, and inadequate headspace under vacuum. The useful working volume should match the smallest and largest planned batch sizes, not just the nameplate capacity.
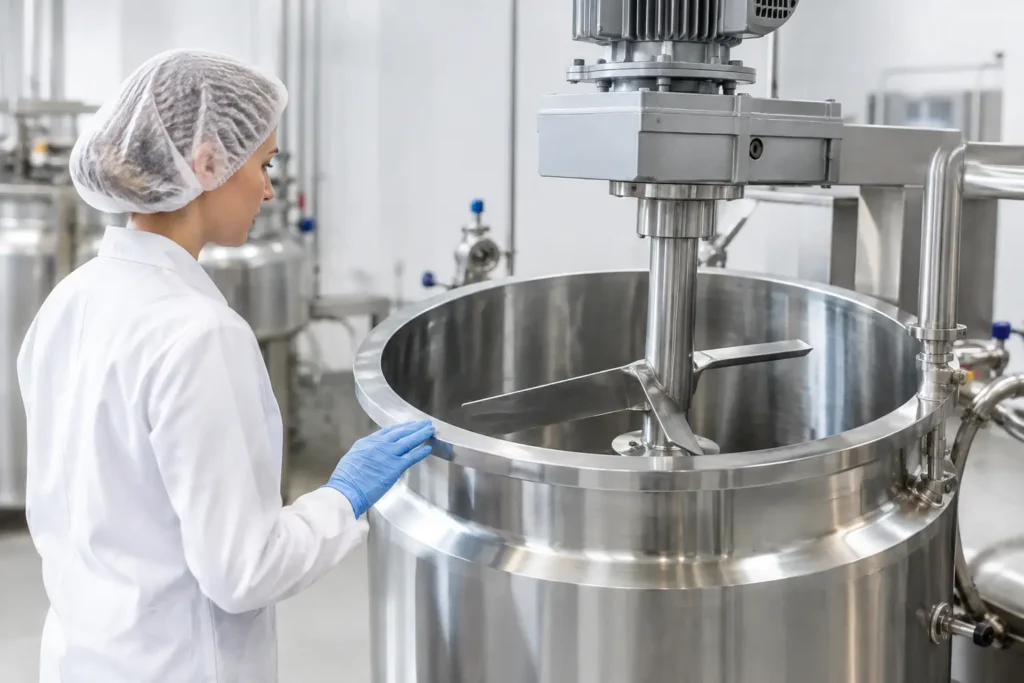
The mixing assembly must solve two jobs at once: create the required product structure and remain accessible to cleaning action. For emulsified foods, an anchor agitator alone may provide wall sweeping and bulk turnover, but it may not deliver the shear needed to disperse oil droplets, hydrate stabilizers, or break powder agglomerates. A rotor-stator homogenizer or inline emulsification stage is often required.
Bottom-entry high-shear units are effective for mayonnaise and dressings because they concentrate shear in the product zone and can reduce the need for external recirculation. However, the seal arrangement, housing geometry, and connection to the vessel must be designed for hygienic service. Mechanical seals should be selected for the operating vacuum, temperature, cleaning chemicals, and expected production schedule. A seal that performs well in water may not perform equally well in hot CIP cycles or abrasive formulations.
For highly viscous products, a close-clearance anchor with scrapers can improve heat transfer and prevent product buildup on vessel walls. The trade-off is that scraper assemblies add components that must be cleaned and inspected. Their material selection, mounting design, and clearances should support both reliable operation and sanitary maintenance.
An effective sanitary mixer design guide also considers the powder path. Dry starches, gums, salt, sugar, and protein powders can form persistent deposits if they enter through an open manway or poorly designed hopper. A closed powder induction system can improve dispersion and reduce dust, but it must be included in the cleaning boundary. Every hose, valve, eductor, filter, and powder contact surface needs a defined CIP or disassembly procedure.
A clean vessel cannot compensate for unsanitary piping, valves, instruments, or transfer equipment. Treat the full process path – from ingredient addition through discharge – as one connected sanitary system.
Use short, drainable piping runs with minimal low points. Where process constraints require low points, provide a drain strategy rather than assuming CIP flow will remove all residue. Dead legs should be minimized through correct valve placement and hygienic branch design. Long instrument stubs, unused ports, and poorly located sample valves can become recurring sanitation weak points.
Valve selection deserves close attention. Butterfly valves may suit simple, low-risk transfer duties, while mixproof or diaphragm-style designs may be preferable where isolation, cleaning segregation, or allergen control is critical. The correct choice depends on the product, cleaning system, operating pressure, and level of process automation. A lower initial valve cost can become expensive if it creates repeated disassembly work or limits cleaning validation.
Instrumentation should support both processing and sanitation. Temperature measurement is needed for thermal control and CIP verification. Vacuum measurement helps manage deaeration and batch consistency. Load cells or accurate level control improve repeatable batching. Conductivity and flow measurement can help verify cleaning solution concentration and circulation performance. The goal is not to add instruments for their own sake, but to build evidence that the system is operating as designed.
CIP success depends on impingement, flow pattern, chemical action, time, and temperature. A static spray ball may be sufficient for some low-viscosity applications, but it is not automatically the right answer for a vessel that handles heavy mayonnaise, starch-thickened dressings, or adhesive sauce bases. Rotary spray devices can provide stronger mechanical action, although they require adequate supply pressure and flow.
Coverage must extend to the vessel walls, lid, agitator shaft, internal attachments, homogenizer housing, discharge valve, recirculation loop, and powder induction components. Vacuum lines and condensers also require evaluation. If product can enter a line during normal operation, that line belongs in the sanitation plan.
Request a documented cleaning concept during equipment design. It should identify the cleaning circuits, supply conditions, drain points, expected cycle stages, and components requiring manual inspection. For high-risk products or complex systems, factories should conduct riboflavin coverage tests, swab testing, and process-specific validation after installation. A successful water test alone does not prove removal of oil-rich or starch-based residues.
Food-contact surfaces are commonly fabricated from stainless steel selected for food processing service, with material grades matched to the product, cleaning chemistry, and plant environment. Surface finish should be specified in measurable terms, not described only as “sanitary.” A smoother finish generally reduces residue retention, but extremely fine finishes may not justify their cost in every non-product-contact location.
Gaskets, elastomers, scraper materials, and seal faces deserve the same scrutiny as the vessel shell. They must tolerate oil, acid, salt, cleaning chemicals, vacuum, temperature cycles, and repeated compression. Materials that swell, crack, or retain odor can undermine an otherwise well-designed system.
Access is the practical test of design quality. Operators need safe access to inspect critical areas, service seals, replace scrapers, and verify cleaning without creating unnecessary exposure or extended downtime. Large openings are useful for maintenance, but every opening must seal reliably and avoid becoming a contamination path. The best design balances hands-on access with closed, repeatable processing.
Food manufacturers should ask equipment suppliers to define sanitary performance in the proposal, not leave it to assumptions after purchase. The specification should identify product range, viscosity, batch size, vacuum requirement, thermal duty, powder handling needs, CIP method, utilities, material standards, surface finish, drainability expectations, and factory acceptance testing.
This is where application-specific engineering matters. PerMix designs vacuum emulsifying systems around the realities of mayonnaise and dressing production, including high-shear emulsification, powder incorporation, deaeration, and hygienic processing. The right configuration depends on the formula portfolio and the operating targets, not on a standard mixer layout.
A sanitary mixer is a production asset, not a stainless-steel container with an agitator. When cleaning, drainage, emulsification, powder handling, and maintenance are engineered together, manufacturers gain a system that protects product quality batch after batch and gives the plant more usable production time.
Get in touch with us today and learn how to we can help your business.